Choosing the right sheet metal manufacturer in China requires more than comparing prices. It demands evidence, technical judgment, and careful communication.
A dependable supplier should show real factory capabilities, experienced engineers, and consistent inspection records. Ask about cutting, bending, welding, stamping, surface treatment, and assembly. Then match those capabilities with your drawings and production volume. A polished website proves very little. Factory videos can also mislead.
Look for measurable details. Can the manufacturer explain material grades clearly? Can it control bend angles within your required tolerance? Does it use calibrated inspection tools, such as vernier calipers, height gauges, and CMM equipment? Request sample parts before approving mass production. Examine their edges, holes, welds, coating, and packaging. Small defects often become expensive delays.
Sheet metal educator Ron Covell has repeatedly emphasized a practical workshop principle: “Measure twice, cut once.” The same principle applies to supplier selection. Confirm tolerances, delivery terms, tooling ownership, inspection procedures, and revision control in writing. Ask how the team handles a failed sample or late material.
A lower quotation may look attractive. It may also conceal weaker steel, rushed inspection, or poor process control. I have seen buyers focus on unit price while ignoring rework, freight delays, and communication gaps. That approach deserves reflection.
The best Chinese manufacturer is not always the cheapest. It is the partner that explains limitations, provides traceable evidence, and improves with feedback. Visit the facility when practical, speak with technical staff, and test the relationship with a controlled order. Trust should be earned gradually.
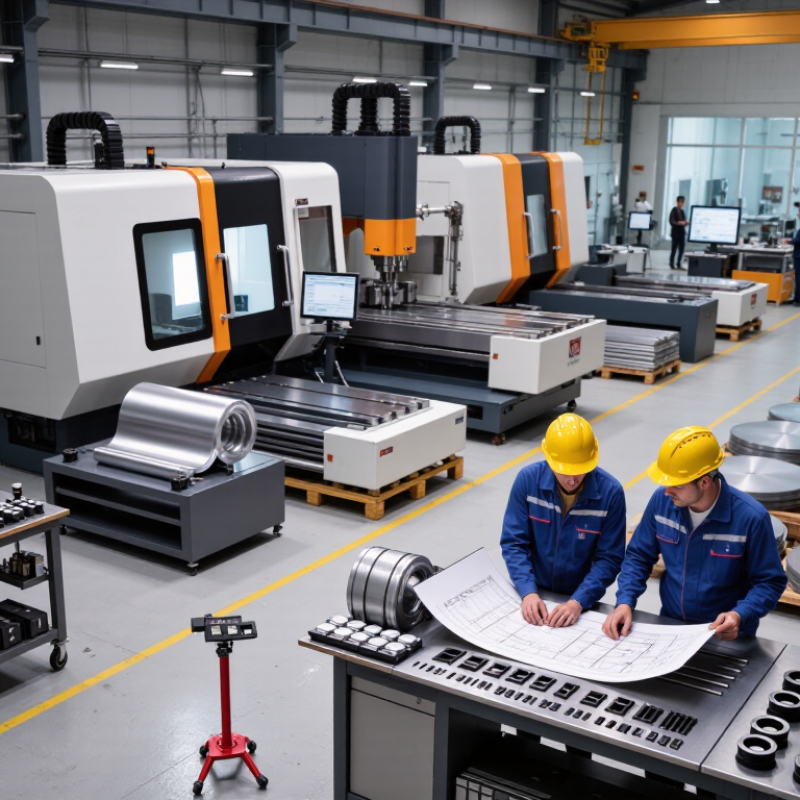
A reliable manufacturer starts with a precise technical brief. State the material grade, thickness, temper, and mechanical requirements. Stainless steel, aluminum, and galvanized steel behave differently during cutting, bending, and welding. Include the finished part dimensions, bend angles, hole locations, and critical reference points. A tolerance of ±0.1 mm sounds clear, but it may be demanding for large panels or welded assemblies. Identify which dimensions truly require it.
Ask how the factory controls these tolerances. Experienced teams should explain their forming sequence, tooling limits, inspection equipment, and process capability. Request inspection records from a similar part, not only a general quality certificate. For example, a coordinate measuring machine can verify hole positions, while calibrated micrometers can check sheet thickness and edge dimensions. One practical lesson is easy to miss: tight tolerances added everywhere can increase cost without improving function.
Tips: Define surface finish with measurable details. Specify brushed direction, powder coating thickness, anodizing requirements, or a target roughness such as Ra 1.6 μm. Add acceptable limits for scratches, dents, discoloration, and weld marks. Ask for a first-article sample before full production. Check it under the lighting used by your customer. Visual standards can remain subjective, even with careful drawings. That part deserves another review.
Finding the best sheet metal manufacturer in China requires more than comparing prices. Inspect the quality system behind each quotation. The ISO Survey 2022 recorded 1,265,216 ISO 9001 certificates worldwide, but certification alone proves limited daily discipline. Request the certificate scope, recent audit findings, corrective-action records, and document-control procedures. Check whether drawings, material grades, and revision changes reach the cutting and bending operators.
PPAP evidence should include dimensional reports, material certificates, process-flow diagrams, control plans, and measurement-system studies. Ask for a real production sample, not a polished presentation. For critical dimensions, request capability charts showing Cpk ≥1.33 from a stable process. Cpk must use specification limits, process average, and actual variation; a single favorable batch can mislead. The Automotive Industry Action Group’s PPAP and SPC guidance supports this evidence-based approach.
I have seen suppliers display ISO certificates while missing revision signatures on shop-floor travelers. Small gaps matter. Visit the factory if possible. Examine burrs, bend marks, mixed material bins, and gauge calibration labels. Check whether operators can explain the reaction plan when Cpk falls below target. Gauge R&R results also deserve attention, because poor measurement can create false confidence. The process may look capable only because the inspection method is weak. Leave room for doubt, and verify production records against the parts in your hands.
How to Find the Best Sheet Metal Manufacturer in China?
Factory capacity should be measured, not accepted from a sales brochure. Laser power affects cutting speed, thickness, and edge quality. However, higher wattage does not guarantee better parts. A 3 kW laser may suit thin stainless steel, while thicker plate may require 6 kW or more. Ask for recent cutting samples, tolerance records, and machine calibration dates. Press tonnage matters equally. A 100-ton press brake can handle many medium-sized bends, but tooling, bend length, material strength, and thickness change the real limit. I once focused on tonnage alone. That was a poor shortcut.
MOQ and lead time reveal factory discipline. A low MOQ can reduce inventory risk, but it may increase setup cost. Request separate figures for sampling, pilot batches, and repeat orders. Define lead time from drawing approval to packed goods, excluding shipping. China’s National Bureau of Statistics reported a manufacturing PMI of 50.1 in December 2024, with the production index at 52.1. This indicates active production, but it does not prove every factory has spare capacity. UNIDO’s 2024 industrial report also highlights productivity and digital capability as major competitiveness factors.
Tips: Compare three written quotations. Record laser wattage, press tonnage, MOQ, and lead time in one table. Ask how many machines are operational today. Check an unfinished batch, not only polished samples. Leave room for mistakes; drawings sometimes hide difficult bends. A factory that explains limitations may be more reliable than one promising everything.
| Factory Profile | Primary Production Focus | Fiber Laser Power | Maximum Sheet Size | Press Brake Tonnage | Typical Material Thickness | Prototype MOQ | Production MOQ | Sample Lead Time | Production Lead Time | Best Fit |
|---|---|---|---|---|---|---|---|---|---|---|
| Profile A | Precision prototypes and low-volume custom parts | 2 kW | 1,500 × 3,000 mm | 100 tons | 0.8–8 mm | 1 piece | 50 pieces | 5–7 working days | 15–20 working days | Engineering validation, samples, and replacement parts |
| Profile B | General industrial enclosures and brackets | 4 kW | 1,500 × 3,000 mm | 160 tons | 1–12 mm | 5 pieces | 100 pieces | 7–10 working days | 20–25 working days | Stable repeat orders with moderate customization |
| Profile C | Medium-volume fabrication for machinery and equipment | 6 kW | 2,000 × 4,000 mm | 250 tons | 1.5–16 mm | 10 pieces | 200 pieces | 10–12 working days | 25–35 working days | Larger components, thicker steel, and repeat production |
| Profile D | High-volume standardized sheet metal components | 8 kW | 2,000 × 6,000 mm | 400 tons | 2–25 mm | 25 pieces | 500 pieces | 12–15 working days | 30–45 working days | Large orders requiring high throughput and consistent output |
| Profile E | Decorative panels, stainless steel parts, and architectural work | 3 kW | 1,500 × 3,000 mm | 130 tons | 0.8–10 mm | 2 pieces | 50 pieces | 7–12 working days | 20–30 working days | Appearance-sensitive products and small-to-medium batches |
How to Find the Best Sheet Metal Manufacturer in China?
Audit cost should be judged against measurable process evidence. Request twelve months of first-pass yield data by material, machine, and product family. A single monthly average can hide repeated rework. There is no universal “good” yield rate for sheet metal. Complex bends and thin gauges naturally create different risks. Verify the calculation: accepted parts divided by total parts produced. Also inspect scrap logs, quarantine areas, weighing records, and corrective-action reports.
The details matter.
A reliable manufacturer should trace each coil or sheet to heat certificates, production orders, and inspection records. Ask whether scrap is segregated by alloy and recorded before disposal. Some factories report high yield but exclude setup waste. That is an uncomfortable question.
Include sampling, laboratory testing, travel, and re-audit expenses in the audit budget. Cheap audits can become expensive surprises.
For regulated products, request a material declaration linked to the bill of materials and homogeneous-material test results. EU RoHS currently restricts ten substances, including lead, mercury, and certain flame retardants, with concentration limits defined by the directive. ECHA reported 247 substances on its REACH Candidate List in June 2025. Supplier declarations must therefore carry revision dates and scope.
ISO 9001 evidence helps, but certification alone proves little about RoHS or REACH control. An effective audit compares certificates with shop-floor labels, purchasing records, and recent test reports.
Finding the best sheet metal manufacturer in China should begin with evidence, not polished factory photos. Ask for a DFM review before signing a contract. The engineer should check bend radii, hole spacing, material thickness, tolerances, and weld access. Request comments directly on your drawings. This reveals whether the team understands real production limits. It may feel slower. It can prevent costly redesigns.
Require a documented first article from the intended material and process. Inspect dimensions, surface finish, deburring, and hole alignment. Ask for measurement records, not only a pass-or-fail statement. Confirm the material certificate and production lot. A first article may look excellent while machine settings remain unstable. In practice, this is where many evaluations become too optimistic. The sample is not the process.
A three-sample run offers stronger evidence. Request three consecutive parts, preferably from normal production conditions. Test their fit with mating components, threaded fasteners, and finishing requirements. Compare critical dimensions across all samples. Small variation matters. Ask how operators control it and what happens after a tool change. If an engineer dismisses a mismatch as harmless, reconsider the supplier. No manufacturer is flawless, but unexplained variation is a warning. Put inspection methods, tolerances, sample approval, and corrective actions into the contract only after reviewing these results.
A DFM review is completed before production and requires no physical sample. A first article uses one manufactured part for initial dimensional and specification verification. A three-sample run checks repeatability across three parts before a larger production commitment.